RoHS & REACH as it applies to printed carbon film heaters: what the document covers, what it deliberately leaves to someone else, and how a made-to-drawing heater is certified at all — which is not the same question as whether a part number is approved.
RoHS & REACH — Scope
Restriction of hazardous substances in the materials and the solder, and declaration of substances of very high concern. Required for anything sold into the EU.
What RoHS & REACH Does Not Cover
A compliance declaration, not a safety approval.
This is the division of labour to carry away from any heating standard: safety standards decide whether the part can hurt somebody, and say nothing about whether it holds a temperature, lasts five years or matches the last batch. Performance is a specification you write; safety is one the standard writes.
How a Made-to-Drawing Heater Is Certified
A construction is built and tested to a standard. The insulation system, the creepage and clearance distances, the earthing, the lead anchorage, the temperature under fault and the marking are what the test covers — and all of those are properties of the construction rather than of the outline it is die-cut to.
So a custom outline does not have a certificate of its own, and no supplier can honestly hand you one. What is available is the construction file: the standard the build is tested to, the materials list with their own ratings, and the test reports. That is what an approvals engineer needs, and it is what the end product's own certification is built on.
The practical consequence: name RoHS & REACH on the enquiry, not after approval. A construction chosen for cost and then asked to pass a standard afterwards usually has to be rebuilt, because the insulation thickness, the creepage distances and the lead anchorage are decided at design time and are not adjustable later.
From the capability table: IEC/EN 60335, UL 94 V-0, RoHS, REACH, CE, IATF 16949.
What a Printed Carbon Film Heaters Is
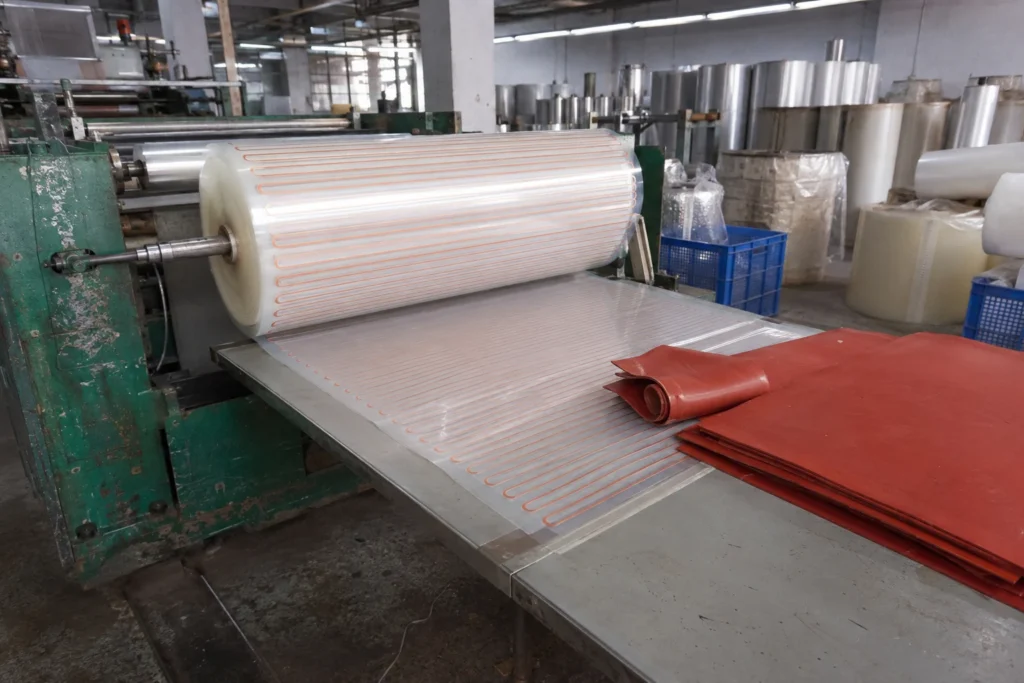
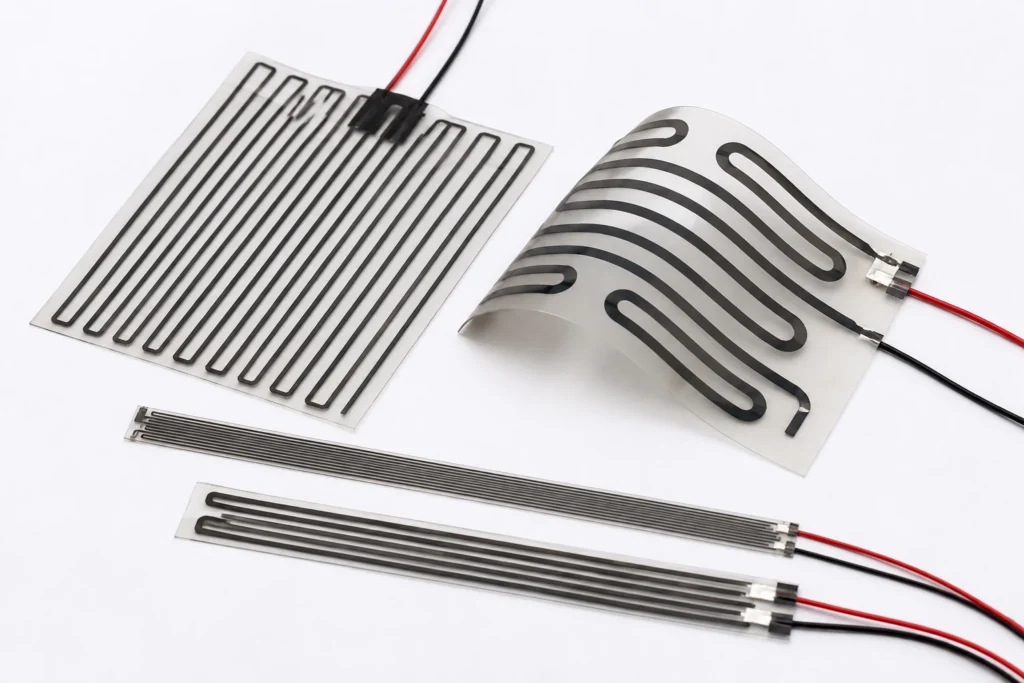
Carbon ink printed on PET: the lowest cost per square metre of any construction here, and the standard answer for large, low watt density heated areas.
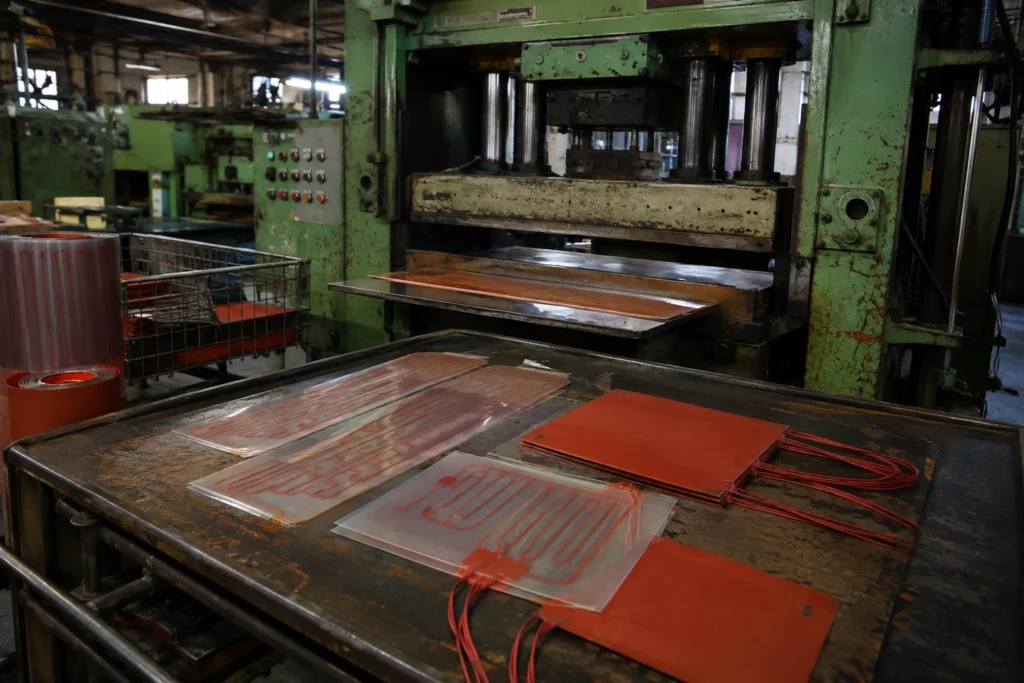
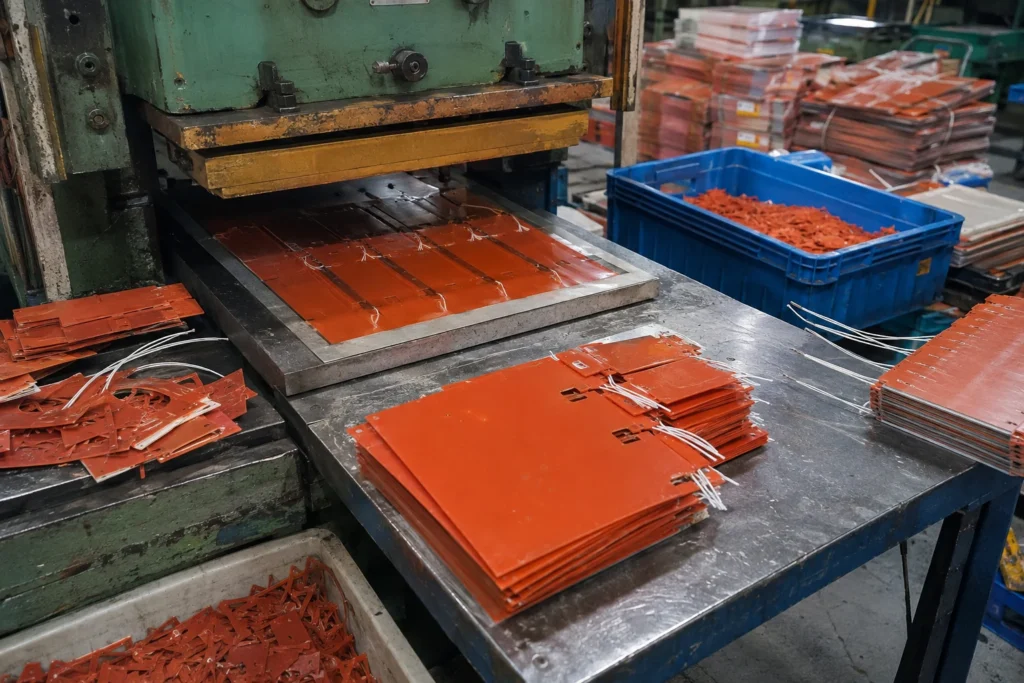
Carbon or silver ink screen printed onto PET polyester film, laminated and die cut. It is made on a roll, which makes it the cheapest heater per square metre by a wide margin at volume, and it stops at 120 °C because the film does.
The heat leaves through the bonded face. Everything that is not in contact with the load radiates and convects from the back of the heater instead, which at these thicknesses is a poor path — so an air gap under part of the outline is not a small loss of efficiency, it is a hot spot at that spot.
| Element | screen-printed carbon or silver ink |
|---|---|
| Insulation system | PET polyester film |
| Total thickness | 0.2 mm |
| Maximum size, one piece | 500 x 1500 mm |
| Continuous working temperature | 120 °C |
The continuous limit of 120 °C is set by PET polyester film. The element alloy would run far hotter; it is never the element that decides.
The Other Standards This Construction Is Built To
A heater is rarely governed by one document. This construction is also built and tested to:
Safety, materials, substances and quality system are four separate questions with four separate documents behind them. A part can satisfy all four and still be the wrong heater for the duty, which is what the rest of this page is about.
Control and Protection
This heater has no way of limiting its own temperature. Resistance heating draws roughly the same power whatever the temperature, so with the load removed, the fluid gone, the fan stopped or the sensor open circuit, the element keeps producing watts until something stops it.
The design must therefore contain a control device and, separately, a protective one: a controller with a sensor to hold the set point, and a bimetal thermostat or a one-shot thermal cutoff wired in series with the element to open the circuit if the loop ever fails. The two are not interchangeable — a controller that has lost its sensor cannot protect anything, which is exactly the fault the cutoff exists for.
PET softens at about 130 °C and loses its dielectric strength as it does, so the cutoff temperature has to sit under that with margin. This is a construction that cannot be allowed to dry out and overshoot.
Sensors can be built into the part: NTC thermistor, PT100 or PT1000 RTD, or a K-type thermocouple, fitted under the same insulation and tested with the heater as one assembly. A sensor laminated into the heater reads the heater; a sensor on the load reads the load. Both are legitimate, and the drawing has to say which is wanted.
Watt Density: the Two Figures
Watt density, not wattage, is what the construction is limited by. 0.1 W/cm² unbonded and 0.5 W/cm² bonded to metal are the limits for this build — so if the wattage is fixed by the duty, the area is what has to move.
Where the required power will not fit into the available area at the free-air figure, the answer is a better thermal path rather than a thinner margin: bond the whole face down, or add a spreader plate. On 150 cm² the difference is roughly 15 W against 75 W, which is usually the whole argument.
Attachment and Thermal Contact
Attachment options are a factory-applied pressure-sensitive adhesive, vulcanising or bonding to the customer's part, or mechanical clamping with a plate or a strap.
A PSA bond wants a clean, dry, degreased surface, continuous pressure while it wets out, and no trapped air: a bubble under the element is a spot with no thermal path, and it will be the first place the heater fails. Acrylic adhesives reach full strength over 24 to 72 hours, so the assembly is not at its rated watt density the moment it is pressed down.
PET film is dimensionally stable enough to laminate into a trim part, and most automotive elements arrive already bonded to their facing rather than as a loose heater.
From the capability table: PSA backing standard; laminated into the end product at high volume.
The bond line is part of the thermal circuit and should be specified like one. A 0.05 mm acrylic PSA layer conducts roughly 0.2 W/m·K; a filled silicone adhesive is two to five times better, and a bolted joint with an interface pad better again. Whatever is chosen, it has to be continuous — the heater cannot spread heat sideways to cover a gap, and the temperature under a void rises until something in the stack gives way.
How to Specify One
This is a made-to-drawing part, so there is no catalogue number to quote. A quotation is built from the following, and the more of it that arrives with the enquiry the fewer rounds it takes:
- An outline drawing, or a sketch with dimensions: overall size, holes, cut-outs, radii and the lead exit position.
- The supply voltage, and whether it is AC or DC. The element is wound for one voltage; it is not a switchable range.
- The power required, or — better — the temperature to be reached and the mass or flow it has to be reached in. Given the second, the wattage can be calculated instead of guessed.
- What the heater is attached to, and how. This is what decides which watt density figure applies, and it is the question a quotation cannot proceed without.
- The ambient, and the lowest temperature the assembly must start from. A heater sized for a 20 °C start is undersized for a -30 °C one.
- Duty cycle: continuous, intermittent, or a warm-up to a deadline. Time to temperature is a specification, not a by-product.
- Sensor and protection: which sensor, where it goes, and which limit device is fitted in series with the element.
- The certification the end product is built to, named on the enquiry rather than after approval.
- Quantity and target price, because the construction that is right for fifty pieces is often not the one that is right for fifty thousand.
- Whether adhesive backing is wanted, and what surface it goes onto — a low-energy plastic needs a different adhesive from bare aluminium.
Lead time: Samples 7-10 days from approved drawing; production 15-20 days.
Printed Carbon Film Heaters — Capability Table
These are process limits for the construction, not the specification of one stocked item. Every line is what the factory can hold; what your part holds is fixed on your drawing.
| Parameter | Specification | Limit / note |
|---|---|---|
| Construction | Carbon-loaded ink screen printed on PET film, silver bus bars, laminated | Decided at quotation from the outline and the wattage |
| Insulation system | PET polyester film, 0.05 mm to 0.125 mm per face | This is what sets the temperature limit, not the element |
| Total thickness | 0.2 mm | Nominal, before adhesive; add 0.2 mm for PSA backing |
| Minimum size | 20 x 20 mm | Below this the element cannot be routed with a safe edge margin |
| Maximum size, one piece | 500 x 1500 mm | Larger areas are supplied as tiled zones with separate circuits |
| Dimensional tolerance | u00b11 mm on the die-cut outline | On the die-cut outline; hole positions are held tighter |
| Supply voltage | 12 V, 24 V, 48 V, 110 V, 220 V | Wound to the ordered voltage u2014 it is not a switchable range |
| Resistance tolerance | u00b110% standard, u00b15% on request | Measured at 20 u00b0C; hot resistance differs with the element alloy |
| Watt density, free air | 0.1 W/cmu00b2 typical | Nothing conducting heat away u2014 the honest figure for an unbonded heater |
| Watt density, bonded to heat sink | 0.5 W/cmu00b2 maximum | Only valid with full-area contact to metal; specifying at this figure and running in free air destroys the heater |
| Continuous working temperature | -40 u00b0C to +120 u00b0C continuous | Of the heater itself, measured at the element, not the ambient |
| Dielectric strength | 1500 V AC, 1 minute | One minute, element to any exposed surface, no breakdown |
| Insulation resistance | greater than 100 Mu03a9 | At 500 V DC, measured after the dielectric test |
| Lead wire | Crimped or soldered leads, or a printed silver bus bar with a bonded tail | Length, gauge and termination to your drawing |
| Attachment | PSA backing standard; laminated into the end product at high volume | Adhesive-backed heaters need continuous contact pressure while curing |
| Sensor and control options | NTC 10K B3950 bonded to the film, or a printed PTC ink track | Fitted under the same insulation and tested as one assembly |
| Certifications available | IEC/EN 60335, UL 94 V-0, RoHS, REACH, CE, IATF 16949 | Constructions are built to these; the certificate covers the construction, not every outline |
| Cost | Roll-to-roll printing u2014 the cheapest heater per square metre at volume | The saving is real above a few thousand pieces and disappears below a few hundred |
| Positive temperature coefficient | Carbon ink resistance rises slightly with temperature | A mild self-limiting effect, not a substitute for a thermostat |
Capability figures are for screen-printed carbon or silver ink on PET polyester film. The +120 °C continuous limit is the film's, and it is a hard limit: PET softens and loses dielectric strength above roughly 130 °C, so this construction is only a candidate where the maximum credible temperature is bounded well below it.