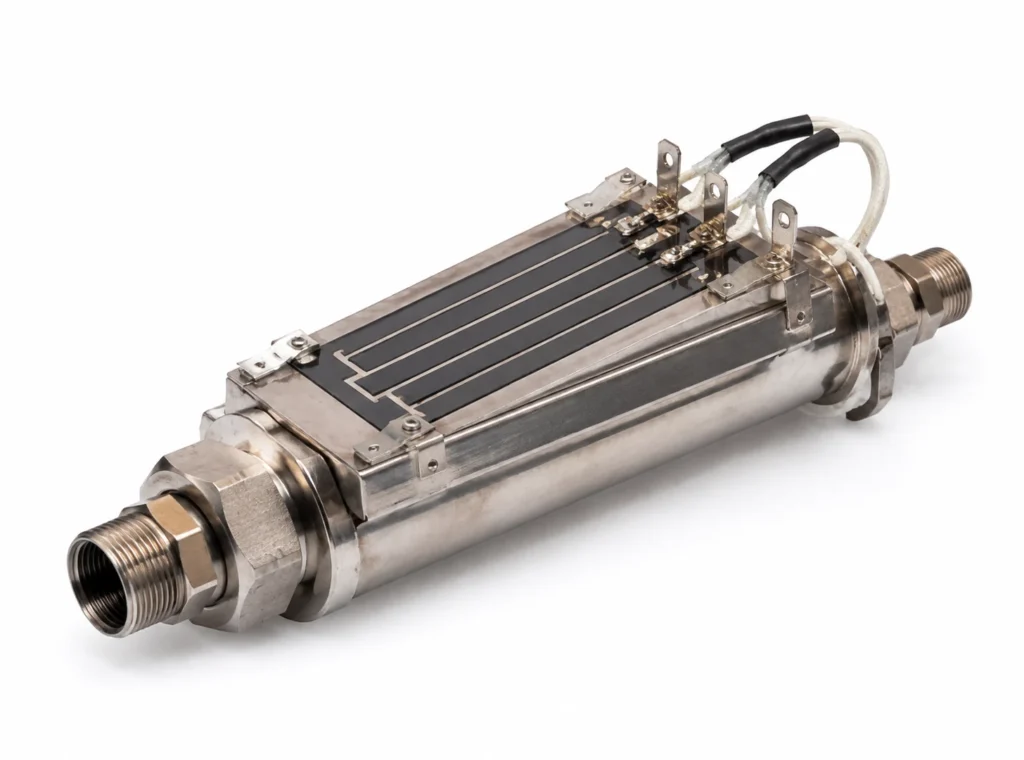
Certification page for instant water heating thick film modules under CE Marking. The manufacturer's declaration that the product meets the applicable EU directives — for a heater, usually the low voltage and EMC directives together with RoHS.
CE Marking — Scope
The manufacturer's declaration that the product meets the applicable EU directives — for a heater, usually the low voltage and EMC directives together with RoHS.
What CE Marking Does Not Cover
CE is self-declared for most heating products; it is not a third-party approval and should not be presented as one.
This is the division of labour to carry away from any heating standard: safety standards decide whether the part can hurt somebody, and say nothing about whether it holds a temperature, lasts five years or matches the last batch. Performance is a specification you write; safety is one the standard writes.
And it is self-declared for most heating products. A CE mark is a manufacturer's statement that the applicable directives have been met, supported by a technical file — it is not a third-party approval, and any supplier presenting it as one is telling you something about themselves.
How a Made-to-Drawing Heater Is Certified
A construction is built and tested to a standard. The insulation system, the creepage and clearance distances, the earthing, the lead anchorage, the temperature under fault and the marking are what the test covers — and all of those are properties of the construction rather than of the outline it is die-cut to.
So a custom outline does not have a certificate of its own, and no supplier can honestly hand you one. What is available is the construction file: the standard the build is tested to, the materials list with their own ratings, and the test reports. That is what an approvals engineer needs, and it is what the end product's own certification is built on.
The practical consequence: name CE Marking on the enquiry, not after approval. A construction chosen for cost and then asked to pass a standard afterwards usually has to be rebuilt, because the insulation thickness, the creepage distances and the lead anchorage are decided at design time and are not adjustable later.
From the capability table: UL 499, IEC/EN 60335, RoHS, REACH, CE.
What an Instant Water Heating Thick Film Modules Is
Flow-through heating modules for coffee machines, water dispensers and sanitary ware, where the water passes over the fired resistor with no tank and no warm-up.
Dielectric and resistor pastes screen printed onto stainless steel or alumina and fired at around 850 °C, then laser trimmed to resistance. There is no separate element and no interface: the heated surface is the substrate itself. In a fluid module the far face is the wetted wall, so the water carries the heat away as fast as the paste produces it — which is what allows watt densities an order of magnitude above any flexible construction, and what makes dry-run protection mandatory rather than advisable.
The heat leaves through a clamped joint, and a clamped joint is only as good as the pressure and the flatness behind it. A thermal interface material or a thin film of thermal grease fills the gaps that machining leaves; without one, contact happens at the high spots and the element runs hotter than the plate it is bolted to.
| Element | fired resistor paste, laser trimmed |
|---|---|
| Insulation system | fired glass dielectric on the substrate |
| Total thickness | 2 mm to 4 mm |
| Maximum size, one piece | 150 x 300 mm |
| Continuous working temperature | 300 °C |
The continuous limit of 300 °C is set by fired glass dielectric on the substrate. The element alloy would run far hotter; it is never the element that decides.
Other Constructions Built to CE Marking
Control and Protection
This heater has no way of limiting its own temperature. Resistance heating draws roughly the same power whatever the temperature, so with the load removed, the fluid gone, the fan stopped or the sensor open circuit, the element keeps producing watts until something stops it.
The design must therefore contain a control device and, separately, a protective one: a controller with a sensor to hold the set point, and a bimetal thermostat or a one-shot thermal cutoff wired in series with the element to open the circuit if the loop ever fails. The two are not interchangeable — a controller that has lost its sensor cannot protect anything, which is exactly the fault the cutoff exists for.
On a fluid heater the limit device belongs on the substrate, close to the resistor, not downstream in the water. Downstream is where the temperature has already gone wrong; the substrate is where it goes wrong first, and at these watt densities the interval between the two is short.
Sensors can be built into the part: NTC thermistor, PT100 or PT1000 RTD, or a K-type thermocouple, fitted under the same insulation and tested with the heater as one assembly. A sensor laminated into the heater reads the heater; a sensor on the load reads the load. Both are legitimate, and the drawing has to say which is wanted.
Watt Density: the Two Figures
Two watt densities are quoted because there are two thermal situations. With nothing conducting heat away, 20 W/cm² is what the insulation survives. Bonded to a heat sink over the full outline, 100 W/cm² is. Anything in between depends on the quality of the joint, and the joint is the customer's to make.
The failure is silent and quick: the element does not know how it is mounted, so at 100 W/cm² in free air the heat simply accumulates in the insulation until it degrades. This is the single most common way these heaters are destroyed, and it happens on the first run rather than after a year.
Thick film reaches these densities because the heated surface is the substrate — there is no interface between element and load to conduct across. That is also why dry-run protection is not optional: with the fluid gone, so is the entire thermal path, and the fired layers reach their limit in seconds rather than minutes.
Leads and Terminations
Termination is specified on the drawing: lead length, gauge, insulation and the connector or tag at the end of it.
Connector and termination options: Welded tabs, crimp terminals or soldered leads depending on temperature. A keyed housing removes a soldering operation from the customer's line and removes the possibility of the assembly being connected backwards; on a heater with a separate sensor circuit it also stops the sensor pair being mistaken for the power pair.
The lead exit is a thermal discontinuity as well as an electrical one. The joint between a fine element and a stranded lead is the hottest point of many heaters, so it is kept out of the highest watt density zone, strain relieved, and — where the exit sits in a hot area — insulated in PTFE rather than in silicone.
How to Specify One
This is a made-to-drawing part, so there is no catalogue number to quote. A quotation is built from the following, and the more of it that arrives with the enquiry the fewer rounds it takes:
- An outline drawing, or a sketch with dimensions: overall size, holes, cut-outs, radii and the lead exit position.
- The supply voltage, and whether it is AC or DC. The element is wound for one voltage; it is not a switchable range.
- The power required, or — better — the temperature to be reached and the mass or flow it has to be reached in. Given the second, the wattage can be calculated instead of guessed.
- What the heater is attached to, and how. This is what decides which watt density figure applies, and it is the question a quotation cannot proceed without.
- The ambient, and the lowest temperature the assembly must start from. A heater sized for a 20 °C start is undersized for a -30 °C one.
- Duty cycle: continuous, intermittent, or a warm-up to a deadline. Time to temperature is a specification, not a by-product.
- Sensor and protection: which sensor, where it goes, and which limit device is fitted in series with the element.
- The certification the end product is built to, named on the enquiry rather than after approval.
- Quantity and target price, because the construction that is right for fifty pieces is often not the one that is right for fifty thousand.
- The fluid, its flow rate and its inlet temperature, and how a dry-run condition is detected in your system.
Lead time: Samples 7-10 days from approved drawing; production 15-20 days.
Instant Water Heating Thick Film Modules — Capability Table
These are process limits for the construction, not the specification of one stocked item. Every line is what the factory can hold; what your part holds is fixed on your drawing.
| Parameter | Specification | Limit / note |
|---|---|---|
| Construction | Glass dielectric and resistor pastes screen printed and fired onto the substrate, then laser trimmed to resistance | Fired, bonded or encapsulated as a single assembly |
| Substrate | 304 stainless flow plate | The substrate carries the heat and the mechanical load |
| Thickness | 2 mm to 4 mm | Substrate plus element system |
| Maximum size, one piece | 150 x 300 mm | Limited by the firing or curing fixture |
| Dimensional tolerance | u00b10.2 mm on the substrate, u00b10.1 mm on printed features | On the machined substrate |
| Supply voltage | 12 V DC to 400 V AC | Circuit is designed for the ordered voltage |
| Resistance tolerance | u00b110% standard, u00b15% selected | Thick film resistors are laser trimmed where a tighter band is required |
| Watt density | 20 W/cmu00b2 typical, 100 W/cmu00b2 maximum in a wetted application | Achievable because the heat is generated in the surface being cooled |
| Maximum working temperature | +300 u00b0C at the element system | Of the element system; the substrate itself tolerates more |
| Dielectric strength | 2500 V AC, 1 minute | One minute, circuit to substrate |
| Insulation resistance | greater than 100 Mu03a9 at 500 V DC | At 500 V DC |
| Terminations | Welded tabs, crimp terminals or soldered leads depending on temperature | Soldered, welded or crimped as the temperature allows |
| Mounting | Bolted, brazed or welded into the assembly; flatness of the mating face is critical | Flatness of the mating face matters more than clamping force |
| Sensor and control options | Printed PTC or NTC track, or a bonded thermocouple | Integrated into the same firing or bonded to the substrate |
| Certifications available | UL 499, IEC/EN 60335, RoHS, REACH, CE | Construction level |
| Flow rate | 0.5 to 6 L/min depending on rise and power | Power required is 70 W per L/min per u00b0C of rise u2014 check the supply before the heater |
| Dry-run protection | Mandatory: NTC or thermal cutoff on the outlet face | A dry thick film plate at 100 W/cmu00b2 fails in seconds, not minutes |
Capability figures are this factory's process limits for fired thick film construction. Watt densities far above any flexible heater are achievable because the resistor is printed directly onto the surface being cooled — there is no interface and no adhesive in the heat path.