A 12 V DC element is not a 230 V AC element with a different label on it — the resistance differs by the square of the ratio, and with it the conductor gauge and the whole circuit layout. This page sets out what 12 V DC does to the design of polyimide heaters with psa backing.
The Element at 12 V DC
Two equations do all the work: P = V²/R and I = P/V. At 12 V DC, 120 W is 1.2 Ω and 10 A.
| Worked example | 120 W at 12 V DC |
|---|---|
| Element resistance, R = V²/P | 1.2 Ω |
| Current, I = P/V | 10 A |
The span matters more than the example. At 12 V DC a 20 W element is 7 Ω and a 500 W element is 0.3 Ω — a factor of twenty-five in resistance, met by changing the conductor cross-section and the length of the path, both of which are constrained by the outline.
At low voltage the difficulty is current, not insulation. 10 A wants 16 AWG rather than 22 AWG lead wire: 16 AWG is about 13 mΩ per metre, so a 2 m pair adds roughly 0.053 Ω to the circuit and dissipates 5.3 W in the leads instead of in the heater. Contact resistance at a crimp or a connector sits in series with the element in exactly the same way, and on a 1 Ω element a 20 mΩ joint is 2% of the power lost where nobody is looking for it.
The design consequence is that lead length and termination are part of the specification at low voltage. On a 5 V element the leads and the connector can account for a tenth of the total resistance, which shows up directly as a heater that never reaches temperature.
Resistance tolerance is u00b110% standard, u00b15% on request, and power follows resistance inversely: a u00b110% standard, u00b15% on request tolerance band is the same band on the delivered wattage. Where the wattage matters — a warm-up to a deadline, a pack of heaters that must match — say so on the enquiry and the tighter band is selected and tested.
Isolation, Earthing and Safety Class
12 V DC is inside the safety extra-low voltage band, so the supply itself is not a shock hazard and the heater does not need a protective earth or double insulation on that account. The low voltage directive does not apply below 75 V DC.
What still applies is everything else: the element is at the far end of a circuit that can deliver a large current, so short-circuit protection, conductor sizing and the thermal cutoff are unchanged. Low voltage removes the shock risk, not the fire risk.
| Dielectric withstand | 1500 V AC, 1 minute (2500 V AC on the 0.125 mm film build) |
|---|---|
| Insulation resistance | greater than 100 Mu03a9 |
Every heater is tested to these before it ships, element to any exposed surface. A dielectric test is a pass or a fail, not a measurement — a part that passes at 2500 V is not one that may be run at 2500 V.
What a Polyimide Heaters with PSA Backing Is
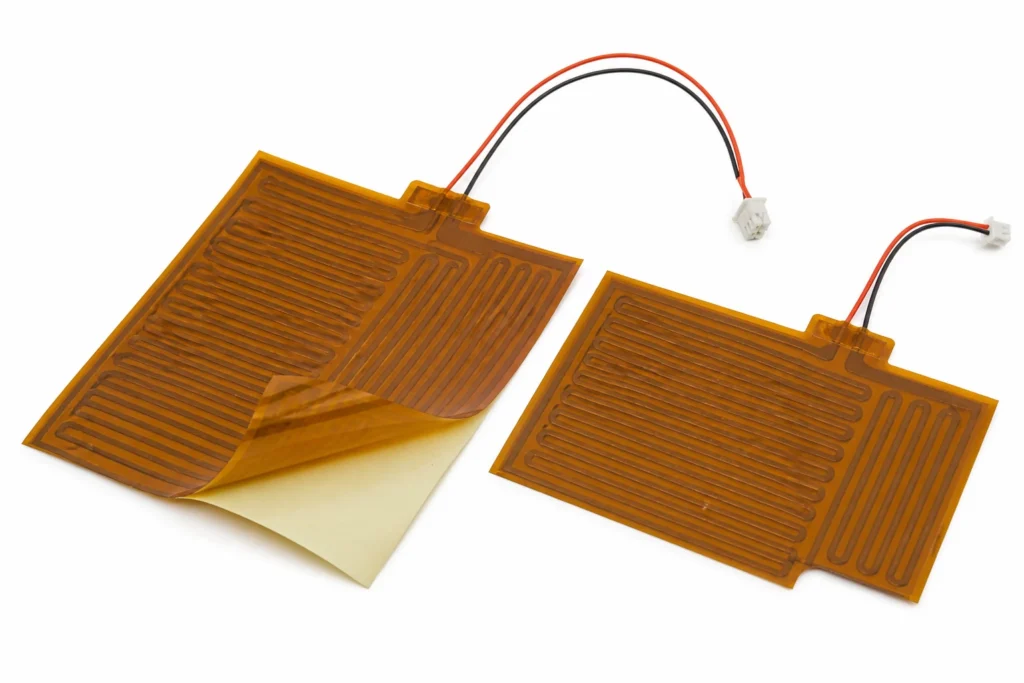
PI heaters supplied with 3M pressure sensitive adhesive and a release liner, for bonding directly to glass, aluminium or a PCB.
A photo-etched copper or Inconel foil circuit laminated between polyimide films, 0.2 to 0.4 mm thick in total. It is the thinnest and fastest flexible heater made: almost no thermal mass of its own, so what it heats is the part rather than itself. Supplied with an acrylic or silicone pressure-sensitive adhesive on one face, which adds about 0.05 to 0.1 mm and becomes the thermal path — the bond line, not the film, is what limits heat out of the heater.
The heat leaves through the bonded face. Everything that is not in contact with the load radiates and convects from the back of the heater instead, which at these thicknesses is a poor path — so an air gap under part of the outline is not a small loss of efficiency, it is a hot spot at that spot.
| Element | photo-etched copper or Inconel foil |
|---|---|
| Insulation system | polyimide film |
| Total thickness | 0.3 mm |
| Maximum size, one piece | 300 x 500 mm (one piece) |
| Continuous working temperature | 200 °C |
The continuous limit of 200 °C is set by polyimide film. The element alloy would run far hotter; it is never the element that decides.
Switching a DC Element
DC has no zero crossing, so a mechanical contact has to break the arc itself. A relay rated 10 A at 250 V AC may be rated 1 A or less at 30 V DC for exactly that reason, and using the AC number is how contacts weld closed — with a resistive heater on the other side, a welded contact is a heater that cannot be turned off. At 12 V DC and 10 A, use a MOSFET, a DC-rated solid state relay or a contactor with a DC rating.
PWM is the natural control method on DC, and a low frequency is right: a few hertz to a few hundred hertz is plenty for something with the thermal time constant of a heater, and it keeps the switching losses and the emissions down. There is nothing to gain from switching a thermal load at 20 kHz.
One DC-specific failure mode is worth naming: a continuous DC bias across a damp printed circuit drives electrochemical migration between adjacent tracks. It is why a silver-ink element in a humid installation is specified with a conformal barrier or reversed periodically, and why carbon ink is still used where the geometry allows it.
Attachment and Thermal Contact
Attachment options are a factory-applied pressure-sensitive adhesive, vulcanising or bonding to the customer's part, or mechanical clamping with a plate or a strap.
A PSA bond wants a clean, dry, degreased surface, continuous pressure while it wets out, and no trapped air: a bubble under the element is a spot with no thermal path, and it will be the first place the heater fails. Acrylic adhesives reach full strength over 24 to 72 hours, so the assembly is not at its rated watt density the moment it is pressed down.
On a 0.2 mm film the adhesive is a meaningful fraction of the total stack and of the thermal resistance. It is also the temperature limit of the assembly in most cases: acrylic PSA is comfortable to about 150 °C, well short of what the polyimide itself will take, so a 200 °C duty needs a silicone adhesive or a bond made by the customer.
From the capability table: Free, 3M PSA backing, or bonded with a two-part thermally conductive adhesive.
The bond line is part of the thermal circuit and should be specified like one. A 0.05 mm acrylic PSA layer conducts roughly 0.2 W/m·K; a filled silicone adhesive is two to five times better, and a bolted joint with an interface pad better again. Whatever is chosen, it has to be continuous — the heater cannot spread heat sideways to cover a gap, and the temperature under a void rises until something in the stack gives way.
Leads and Terminations
Lead wire as supplied: PTFE or silicone insulated 24 AWG to 20 AWG, or an FFC tail etched as part of the circuit. Length, gauge, exit position and termination are drawing items — the exit position in particular, because it decides where the heater can be routed and it cannot be changed after the tool is cut.
The lead exit is a thermal discontinuity as well as an electrical one. The joint between a fine element and a stranded lead is the hottest point of many heaters, so it is kept out of the highest watt density zone, strain relieved, and — where the exit sits in a hot area — insulated in PTFE rather than in silicone.
On a 0.2 mm film the lead joint is thicker than the heater. Where the assembly has to stay flat, the leads are brought out to a tail or a flat flexible tab rather than soldered onto the heated area.
Control and Protection
This heater has no way of limiting its own temperature. Resistance heating draws roughly the same power whatever the temperature, so with the load removed, the fluid gone, the fan stopped or the sensor open circuit, the element keeps producing watts until something stops it.
The design must therefore contain a control device and, separately, a protective one: a controller with a sensor to hold the set point, and a bimetal thermostat or a one-shot thermal cutoff wired in series with the element to open the circuit if the loop ever fails. The two are not interchangeable — a controller that has lost its sensor cannot protect anything, which is exactly the fault the cutoff exists for.
Sensors can be built into the part: NTC thermistor, PT100 or PT1000 RTD, or a K-type thermocouple, fitted under the same insulation and tested with the heater as one assembly. A sensor laminated into the heater reads the heater; a sensor on the load reads the load. Both are legitimate, and the drawing has to say which is wanted.
How This Construction Fails
- Run at the bonded watt density in free air. The insulation reaches its limit within minutes and the element burns through where the local density is highest. Specify at 5 W/cm² only where the heater is genuinely bonded to metal over its whole area; unbonded, the figure is 0.5 W/cm².
- Voids under the bond. Air trapped during application, a contaminated surface or an adhesive that never reached full cure all produce the same result: a patch with no thermal path, running far above the rest of the heater, which is where the failure starts.
- Loss of the control loop. An open-circuit sensor, a welded relay contact or a controller in manual leaves the element at full power with nothing watching it — the case the series thermal cutoff exists for, and the reason it must not be omitted to save a part.
- A nick in the film. Polyimide tears from a defect at the edge, so sharp internal corners and hand-trimmed outlines both propagate. It also hydrolyses in continuous steam, which rules out sterilisation duty for the bare film.
How to Specify One
This is a made-to-drawing part, so there is no catalogue number to quote. A quotation is built from the following, and the more of it that arrives with the enquiry the fewer rounds it takes:
- An outline drawing, or a sketch with dimensions: overall size, holes, cut-outs, radii and the lead exit position.
- The supply voltage, and whether it is AC or DC. The element is wound for one voltage; it is not a switchable range.
- The power required, or — better — the temperature to be reached and the mass or flow it has to be reached in. Given the second, the wattage can be calculated instead of guessed.
- What the heater is attached to, and how. This is what decides which watt density figure applies, and it is the question a quotation cannot proceed without.
- The ambient, and the lowest temperature the assembly must start from. A heater sized for a 20 °C start is undersized for a -30 °C one.
- Duty cycle: continuous, intermittent, or a warm-up to a deadline. Time to temperature is a specification, not a by-product.
- Sensor and protection: which sensor, where it goes, and which limit device is fitted in series with the element.
- The certification the end product is built to, named on the enquiry rather than after approval.
- Quantity and target price, because the construction that is right for fifty pieces is often not the one that is right for fifty thousand.
- Whether adhesive backing is wanted, and what surface it goes onto — a low-energy plastic needs a different adhesive from bare aluminium.
Lead time: Samples 7-10 days from approved drawing; production 15-20 days.
Polyimide Heaters with PSA Backing — Capability Table
These are process limits for the construction, not the specification of one stocked item. Every line is what the factory can hold; what your part holds is fixed on your drawing.
| Parameter | Specification | Limit / note |
|---|---|---|
| Construction | Photo-etched copper or Inconel foil circuit laminated between polyimide films with a high temperature acrylic or FEP adhesive | Decided at quotation from the outline and the wattage |
| Insulation system | Polyimide film, 0.05 mm or 0.125 mm per face | This is what sets the temperature limit, not the element |
| Total thickness | 0.3 mm | Nominal, before adhesive; add 0.2 mm for PSA backing |
| Minimum size | 10 x 10 mm | Below this the element cannot be routed with a safe edge margin |
| Maximum size, one piece | 300 x 500 mm (one piece) | Larger areas are supplied as tiled zones with separate circuits |
| Dimensional tolerance | u00b10.5 mm on dimensions up to 200 mm | On the die-cut outline; hole positions are held tighter |
| Supply voltage | 5 V DC to 240 V AC, wound to order | Wound to the ordered voltage u2014 it is not a switchable range |
| Resistance tolerance | u00b110% standard, u00b15% on request | Measured at 20 u00b0C; hot resistance differs with the element alloy |
| Watt density, free air | 0.5 W/cmu00b2 typical, 0.8 W/cmu00b2 maximum | Nothing conducting heat away u2014 the honest figure for an unbonded heater |
| Watt density, bonded to heat sink | 5.0 W/cmu00b2 maximum | Only valid with full-area contact to metal; specifying at this figure and running in free air destroys the heater |
| Continuous working temperature | -200 u00b0C to +200 u00b0C continuous (+220 u00b0C short term) | Of the heater itself, measured at the element, not the ambient |
| Dielectric strength | 1500 V AC, 1 minute (2500 V AC on the 0.125 mm film build) | One minute, element to any exposed surface, no breakdown |
| Insulation resistance | greater than 100 Mu03a9 | At 500 V DC, measured after the dielectric test |
| Lead wire | PTFE or silicone insulated 24 AWG to 20 AWG, or an FFC tail etched as part of the circuit | Length, gauge and termination to your drawing |
| Attachment | Free, 3M PSA backing, or bonded with a two-part thermally conductive adhesive | Adhesive-backed heaters need continuous contact pressure while curing |
| Sensor and control options | NTC 10K B3950, PT100/PT1000, K-type thermocouple, KSD9700 bimetal thermostat, thermal cutoff | Fitted under the same insulation and tested as one assembly |
| Certifications available | UL 499 construction, IEC/EN 60335, UL 94 V-0, RoHS, REACH, CE, ISO 13485 QMS | Constructions are built to these; the certificate covers the construction, not every outline |
| Adhesive | 3M 966 (to +230 u00b0C), 468MP (to +150 u00b0C) or 9077 | The high temperature acrylics keep the assembly within the film's own rating |
| Application | Roll on from one edge with a squeegee, above +15 u00b0C | Trapped air under a 0.25 mm heater is a visible bubble and a real hot spot |
Capability figures are this factory's process limits for etched-foil polyimide construction. The 200 °C continuous limit and the watt density ceiling (to about 7.75 W/cm² with heat sinking) are properties of the polyimide film and the adhesive system, and are published consistently across the industry.