Duty temperature decides the construction before anything else does. At 150 °c to 200 °c, medical device polyimide heaters is a candidate; the sections below set out what it will hold, what has to be true for it to hold it, and what fails first when it does not.
What the 150 °C to 200 °C Band Requires
The top of the flexible polymer range. Silicone rubber and polyimide both run continuously at 200 °C; above it both degrade, and no amount of derating changes that.
| Band | 150 °C to 200 °C |
|---|---|
| This construction, continuous | 200 °C |
| Limited by | polyimide film |
This band reaches the ceiling of the construction. At 200 °C there is no headroom left, so the control has to hold the set point rather than approach it from above, and the limit device has to be set where it can act before the insulation does. A duty that spends its time at the top of the band is a duty that should be quoted against the next construction up.
Why the Boundary Is Where It Is
200 °C is the top of the flexible polymer range. Silicone rubber and polyimide both run there continuously, and both degrade above it — silicone hardens and loses its tear strength, polyimide embrittles. No derating changes either.
Cross this line and the construction changes completely: fired thick film on stainless or alumina, or a mica-insulated element. Those parts are rigid, clamped and made to a different drawing, so the boundary is a redesign rather than a substitution.
What a Medical Device Polyimide Heaters Is
PI heaters built under an ISO 13485 quality system for diagnostic instruments, sample warming, reagent cartridges and patient-contact assemblies.
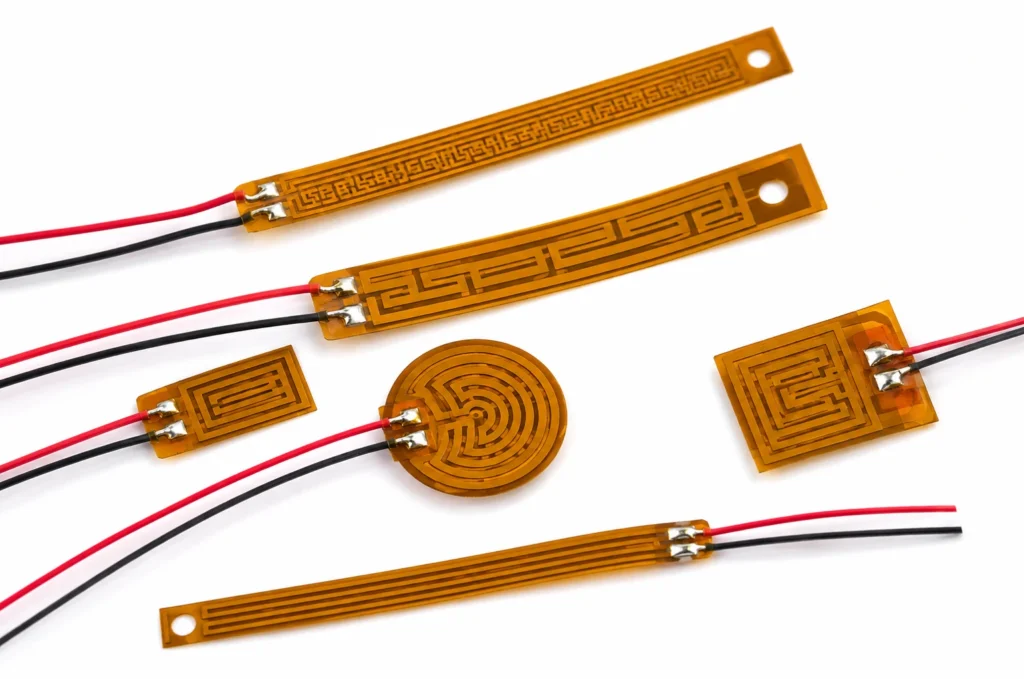
A photo-etched copper or Inconel foil circuit laminated between polyimide films, 0.2 to 0.4 mm thick in total. It is the thinnest and fastest flexible heater made: almost no thermal mass of its own, so what it heats is the part rather than itself. It will wrap a cylinder; it will not take a compound curve, and a nick in a 0.05 mm film propagates from the edge, so outlines are drawn with radiused corners.
The heat leaves through the bonded face. Everything that is not in contact with the load radiates and convects from the back of the heater instead, which at these thicknesses is a poor path — so an air gap under part of the outline is not a small loss of efficiency, it is a hot spot at that spot.
| Element | photo-etched copper or Inconel foil |
|---|---|
| Insulation system | polyimide film |
| Total thickness | 0.25 mm |
| Maximum size, one piece | 300 x 500 mm (one piece) |
| Continuous working temperature | 200 °C |
The continuous limit of 200 °C is set by polyimide film. The element alloy would run far hotter; it is never the element that decides.
Which Temperature Is Being Held
Three temperatures matter and they are not the same number: the element temperature, the temperature of the surface being heated, and the ambient. A heater rated for a continuous working temperature is rated at the element — the hottest point in the assembly, and the one nothing on the outside is measuring.
The gap between element and surface is the thermal path. Bonded to metal it may be a few degrees; across an air gap, a void in the adhesive or a dry clamped joint it can be tens of degrees, and every one of them appears at the element rather than at the load.
Which is why sensor position is a drawing item. A sensor laminated into the heater protects the heater; a sensor on the load controls the load. Assemblies that have to do both carry two: a control sensor where the process is, and a limit device against the element.
Watt Density: the Two Figures
Two watt densities are quoted because there are two thermal situations. With nothing conducting heat away, 0.5 W/cm² is what the insulation survives. Bonded to a heat sink over the full outline, 5 W/cm² is. Anything in between depends on the quality of the joint, and the joint is the customer's to make.
The failure is silent and quick: the element does not know how it is mounted, so at 5 W/cm² in free air the heat simply accumulates in the insulation until it degrades. This is the single most common way these heaters are destroyed, and it happens on the first run rather than after a year.
Control and Protection
This heater has no way of limiting its own temperature. Resistance heating draws roughly the same power whatever the temperature, so with the load removed, the fluid gone, the fan stopped or the sensor open circuit, the element keeps producing watts until something stops it.
The design must therefore contain a control device and, separately, a protective one: a controller with a sensor to hold the set point, and a bimetal thermostat or a one-shot thermal cutoff wired in series with the element to open the circuit if the loop ever fails. The two are not interchangeable — a controller that has lost its sensor cannot protect anything, which is exactly the fault the cutoff exists for.
Sensors can be built into the part: NTC thermistor, PT100 or PT1000 RTD, or a K-type thermocouple, fitted under the same insulation and tested with the heater as one assembly. A sensor laminated into the heater reads the heater; a sensor on the load reads the load. Both are legitimate, and the drawing has to say which is wanted.
How This Construction Fails
- Run at the bonded watt density in free air. The insulation reaches its limit within minutes and the element burns through where the local density is highest. Specify at 5 W/cm² only where the heater is genuinely bonded to metal over its whole area; unbonded, the figure is 0.5 W/cm².
- Voids under the bond. Air trapped during application, a contaminated surface or an adhesive that never reached full cure all produce the same result: a patch with no thermal path, running far above the rest of the heater, which is where the failure starts.
- Loss of the control loop. An open-circuit sensor, a welded relay contact or a controller in manual leaves the element at full power with nothing watching it — the case the series thermal cutoff exists for, and the reason it must not be omitted to save a part.
- A nick in the film. Polyimide tears from a defect at the edge, so sharp internal corners and hand-trimmed outlines both propagate. It also hydrolyses in continuous steam, which rules out sterilisation duty for the bare film.
Where This Construction Is the Wrong Answer
- Do not plan on running above 200 °C. That ceiling belongs to the insulation system, not to the element alloy, and it is not a figure that derating extends — past it the insulation degrades and the dielectric strength goes with it.
- Do not specify polyimide for continuous steam or repeated autoclave cycles — it hydrolyses. Do not fold it to a tight radius, and do not put a sharp internal corner on the outline.
- Do not rely on the insulation as a seal in a wet installation. Where washdown or condensation is expected, the assembly is sealed at the edge and at the lead exit, and both are drawing items.
How to Specify One
This is a made-to-drawing part, so there is no catalogue number to quote. A quotation is built from the following, and the more of it that arrives with the enquiry the fewer rounds it takes:
- An outline drawing, or a sketch with dimensions: overall size, holes, cut-outs, radii and the lead exit position.
- The supply voltage, and whether it is AC or DC. The element is wound for one voltage; it is not a switchable range.
- The power required, or — better — the temperature to be reached and the mass or flow it has to be reached in. Given the second, the wattage can be calculated instead of guessed.
- What the heater is attached to, and how. This is what decides which watt density figure applies, and it is the question a quotation cannot proceed without.
- The ambient, and the lowest temperature the assembly must start from. A heater sized for a 20 °C start is undersized for a -30 °C one.
- Duty cycle: continuous, intermittent, or a warm-up to a deadline. Time to temperature is a specification, not a by-product.
- Sensor and protection: which sensor, where it goes, and which limit device is fitted in series with the element.
- The certification the end product is built to, named on the enquiry rather than after approval.
- Quantity and target price, because the construction that is right for fifty pieces is often not the one that is right for fifty thousand.
- Whether adhesive backing is wanted, and what surface it goes onto — a low-energy plastic needs a different adhesive from bare aluminium.
Lead time: Samples 7-10 days from approved drawing; production 15-20 days.
Medical Device Polyimide Heaters — Capability Table
These are process limits for the construction, not the specification of one stocked item. Every line is what the factory can hold; what your part holds is fixed on your drawing.
| Parameter | Specification | Limit / note |
|---|---|---|
| Construction | Photo-etched copper or Inconel foil circuit laminated between polyimide films with a high temperature acrylic or FEP adhesive | Decided at quotation from the outline and the wattage |
| Insulation system | Polyimide film, 0.05 mm or 0.125 mm per face | This is what sets the temperature limit, not the element |
| Total thickness | 0.25 mm | Nominal, before adhesive; add 0.2 mm for PSA backing |
| Minimum size | 10 x 10 mm | Below this the element cannot be routed with a safe edge margin |
| Maximum size, one piece | 300 x 500 mm (one piece) | Larger areas are supplied as tiled zones with separate circuits |
| Dimensional tolerance | u00b10.5 mm on dimensions up to 200 mm | On the die-cut outline; hole positions are held tighter |
| Supply voltage | 5 V DC to 240 V AC, wound to order | Wound to the ordered voltage u2014 it is not a switchable range |
| Resistance tolerance | u00b110% standard, u00b15% on request | Measured at 20 u00b0C; hot resistance differs with the element alloy |
| Watt density, free air | 0.5 W/cmu00b2 typical, 0.8 W/cmu00b2 maximum | Nothing conducting heat away u2014 the honest figure for an unbonded heater |
| Watt density, bonded to heat sink | 5.0 W/cmu00b2 maximum | Only valid with full-area contact to metal; specifying at this figure and running in free air destroys the heater |
| Continuous working temperature | -200 u00b0C to +200 u00b0C continuous (+220 u00b0C short term) | Of the heater itself, measured at the element, not the ambient |
| Dielectric strength | 1500 V AC, 1 minute (2500 V AC on the 0.125 mm film build) | One minute, element to any exposed surface, no breakdown |
| Insulation resistance | greater than 100 Mu03a9 | At 500 V DC, measured after the dielectric test |
| Lead wire | PTFE or silicone insulated 24 AWG to 20 AWG, or an FFC tail etched as part of the circuit | Length, gauge and termination to your drawing |
| Attachment | Free, 3M PSA backing, or bonded with a two-part thermally conductive adhesive | Adhesive-backed heaters need continuous contact pressure while curing |
| Sensor and control options | NTC 10K B3950, PT100/PT1000, K-type thermocouple, KSD9700 bimetal thermostat, thermal cutoff | Fitted under the same insulation and tested as one assembly |
| Certifications available | UL 499 construction, IEC/EN 60335, UL 94 V-0, RoHS, REACH, CE, ISO 13485 QMS | Constructions are built to these; the certificate covers the construction, not every outline |
| Documentation | Material declarations, lot traceability, and PPAP-equivalent submission | The paperwork is the deliverable as much as the heater is |
| Cleanliness | Assembled and packed in a controlled area; ionic contamination controlled | Specify the cleanliness requirement u2014 it changes the process, not just the packaging |
Capability figures are this factory's process limits for etched-foil polyimide construction. The 200 °C continuous limit and the watt density ceiling (to about 7.75 W/cm² with heat sinking) are properties of the polyimide film and the adhesive system, and are published consistently across the industry.